How to Avoid Poor Adhesion Problems: A Comprehensive Guide
The mechanical boundary where two disparate phases intersect represents one of the most structurally vulnerable zones in modern material engineering, manufacturing assembly, and protective coating technology. Whether examining structural epoxies bonding composite aerospace skins, multi-layer powder coatings curing onto heavy-duty automotive chassis, or specialized pressure-sensitive adhesives securing medical monitors to biological tissue, the integrity of this micro-interlayer dictates total system performance. When boundary integration breaks down prematurely, the resulting delamination triggers consequences that scale from minor cosmetic blemishes to catastrophic structural failures.
In industrial environments, surface interaction physics governs everything from packaging lines to skyscraper curtain walls. Disparate chemical compositions, surface energy differentials, and microscopic contamination layers constantly conspire to undermine bonds between substrates and their applied films or sealants. Traditional troubleshooting protocols frequently treat interfacial separation as an isolated anomaly caused by a single rogue variable—such as an out-of-spec chemical batch, an undertrained technician, or a miscalibrated cure oven. In practice, boundary delamination is rarely isolated; it represents the cumulative physical manifestation of microscopic variables across surface preparation, environmental exposure, and material rheology.
Mastering boundary stability requires moving past superficial remedies like changing solvent wipes or tweaking clamp pressures. Addressing interface vulnerability demands a comprehensive analytical framework that simultaneously evaluates surface energetics, molecular wetting kinetics, environmental microclimates, and cross-linking dynamics. Without this multidisciplinary depth, engineering teams find themselves trapped in expensive cycles of trial-and-error corrections that fail to address the underlying root causes of boundary breakdown.
Understanding how to avoid poor adhesion problems
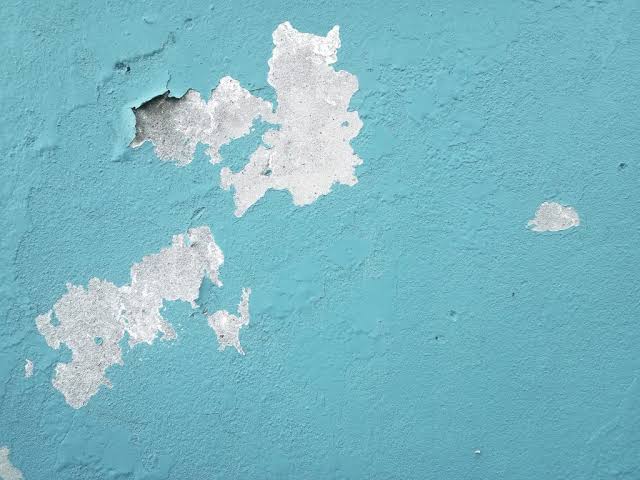
The exact phrase how to avoid poor adhesion problems appears across technical specifications, engineering manuals, and manufacturing forums worldwide. Yet, its practical execution is frequently obscured by generalized guidelines that treat all bonding substrates as uniform, interchangeable surfaces. At its core, mastering how to avoid poor adhesion problems involves controlling surface energy states, eliminating microscopic boundary contamination, matching adhesive rheology to joint geometry, and stabilizing curing microclimates.
A pervasive misunderstanding frames bond failure as an intrinsic chemical deficiency within the adhesive formulation itself. In industrial practice, cohesive failures—where the adhesive splits internally—are relatively rare compared to adhesive failures, where the bond cleanly shears away from the substrate surface. This distinction highlights that boundary separation is fundamentally a surface preparation and thermodynamic issue, not merely a product selection error. When a protective coating delaminates from a metal panel, blaming the coating manufacturer typically ignores the invisible oxide layer, residual machining oils, or moisture film trapped at the interface prior to application.
Oversimplification risks also plague popular technical discourse, which often reduces surface preparation to manual degreasing with a generic solvent. While removing gross grease is essential, modern engineering materials—such as high-strength aluminum alloys, engineered plastics, and carbon-fiber composites—require precise mechanical activation, chemical priming, or plasma treatment to alter surface topography and energy states. Consequently, understanding how to avoid poor adhesion problems requires structural rigor across the entire pre-treatment, application, and curing continuum.
Deep Contextual Background
The evolution of surface bonding mirrors the transition from mechanical fastening (rivets, bolts, and welds) to continuous chemical joining across industrial sectors over the past century. Historically, manufacturing relied heavily on mechanical interlocks because reliable, high-strength synthetic adhesives did not exist. Early bonding agents were limited to natural glues, bitumens, and crude rubber solutions characterized by low environmental resistance and unpredictable creep behavior under sustained loads.
The rapid development of synthetic polymers during and after World War II revolutionized structural joining. Epoxies, polyurethanes, cyanoacrylates, and acrylic systems introduced the possibility of distributing stress evenly across an entire joint area rather than concentrating it at fastener stress concentration points. However, these advanced polymers exposed a steep learning curve: unlike mechanical fasteners that rely on physical capture, synthetic adhesives depend entirely on intimate molecular contact between distinct phases. Early industrial adopters frequently experienced catastrophic delamination because production lines lacked the precise cleaning, priming, and curing controls required to achieve true boundary wetting.
Concurrently, the emergence of lightweighting imperatives in automotive, aerospace, and electronics manufacturing accelerated the adoption of dissimilar material joining—such as bonding carbon composites to aluminum or glass to galvanized steel. Each substrate brings unique surface energies, thermal expansion coefficients, and corrosion vulnerabilities to the interface. Modern regulatory demands, including zero-defect mandates and extended product warranty requirements, have elevated surface engineering from an empirical craft to an exact science governed by strict metrology, automated plasma cleaning, and real-time cure monitoring.
Conceptual Frameworks and Mental Models
Navigating boundary stability requires robust mental models that structure how engineers analyze interfacial mechanics and environmental interactions.
Thermodynamic Work of Adhesion
This model evaluates bonding through the lens of surface free energy and contact angle measurement. For an adhesive to bond effectively, its surface tension must be lower than the critical surface energy of the substrate, allowing the liquid to spontaneously wet microscopic surface irregularities.
-
Limits: Focuses exclusively on initial thermodynamic equilibrium, failing to account for post-cure stress concentrations or chemical degradation over time.
The Weak Boundary Layer Theory
Pioneered by materials scientists, this model posits that interface failure is almost invariably caused by a microscopic weak boundary layer—such as weak oxides, low-molecular-weight fractions, or contamination films—that separates the bulk substrate from the bulk adhesive.
-
Limits: Can overemphasize chemical purity while underestimating mechanical interlocking contributions on rough or porous surfaces.
Diffusion and Interdiffusion Theory
This framework applies primarily to elastomeric and polymeric substrates, where polymer chains from the adhesive cross the interface and entangle with the chains of the substrate, forming a co-mingled boundary zone.
-
Limits: Inapplicable to inorganic substrates like glass, ceramics, and untreated metals that lack mobile polymer chains.
Kinetic Cure Stress Modeling
This model tracks how exothermic reactions, volumetric shrinkage, and thermal gradients during cross-linking generate internal mechanical stresses that pull at the interface during the transition from liquid to solid.
-
Limits: Requires complex computational fluid dynamics and kinetic data that are frequently unavailable for proprietary adhesive formulations.
Key Categories or Variations
Adhesion vulnerabilities manifest differently depending on the material pairing, environmental exposure, and application method. Categorizing these variations clarifies where preventive engineering must focus.
| Substrate Pairing | Primary Failure Mechanism | Dominant Root Cause | Effective Preventive Intervention |
| Metal-to-Metal (Aluminum to Steel) | Galvanic corrosion-induced delamination | Moisture ingress, incompatible electrode potentials | Conversion coatings, chromate-free primers, edge sealing |
| Composite-to-Metal | Interfacial shear failure under thermal cycling | Mismatched coefficients of thermal expansion (CTE) | Flexible toughened epoxy adhesives, controlled ramp rates |
| Plastic-to-Plastic (Polypropylene) | Adhesive peeling due to low surface energy | Lack of polar chemical groups on non-polar surfaces | Corona discharge, flame treatment, specialized primers |
| Glass-to-Metal | UV degradation of interfacial bond line | Photolytic breakdown of silane coupling agents | UV-blocker interlayers, weathering-resistant structural silicones |
| Elastomer-to-Metal | Shock-induced peel failure | Improper vulcanization priming or surface scale | Grit blasting, solvent degreasing, chemical bonding agents |
| Wood-to-Synthetic Polymer | Moisture-induced volumetric swelling stress | Hygroscopic dimensional movement of wood fibers | Moisture-resistant polyurethane glues, sealed substrates |
Realistic Decision Logic for Categorization
When an organization seeks to implement structural bonding protocols, it must first categorize its material pairing and baseline surface energy. High-surface-energy metals require rigorous cleaning and corrosion inhibition, whereas low-surface-energy plastics demand physical or chemical surface activation before any adhesive is introduced. Applying a uniform bonding protocol across dissimilar categories guarantees premature field failures.
Detailed Real-World Scenarios
To understand how adhesion engineering functions in practice, consider four distinct operational environments governed by unique physical constraints and failure modes.
A : Aerospace Composite Assembly
-
Context: Bonding carbon-fiber-reinforced polymer (CFRP) skin panels to aluminum stringers for commercial aircraft wing structures.
-
Constraints: Stringent FAA airworthiness certifications, extreme thermal cycling (-55°C to +85°C), high shear load requirements.
-
Decision Points: Choosing between peel-ply surface preparation fabrics versus automated abrasive grit blasting prior to structural epoxy application.
-
Failure Modes: Leaving residual release agents from the peel-ply fabric on the composite surface due to inadequate solvent wiping, resulting in interlaminar boundary shear under aerodynamic flutter.
-
Second-Order Effects: Adopting automated atmospheric plasma cleaning eliminates chemical solvent waste and improves bond repeatability, but requires high capital expenditure and tight robotic pathway programming.
B : Automotive Exterior Trim Bonding
-
Context: Securing painted thermoplastic olefin (TPO) body side moldings to automotive painted steel bodies using acrylic foam tape.
-
Constraints: High-speed assembly line takt times, variable ambient factory temperatures, resistance to carwash pressure washers and road salts.
-
Decision Points: Evaluating manual wipe primer application versus automated robotic primer jetting with inline optical inspection.
-
Failure Modes: Applying tape to body panels that have cooled below the dew point, trapping microscopic condensation films that hydrolyze the acrylic adhesive interface over time.
-
Second-Order Effects: Implementing mandatory thermal stabilization zones on the assembly line prevents condensation-induced delamination, but expands plant footprint and increases energy consumption.
C : Medical Device Housing Sealing
-
Context: UV-curing a polycarbonate diagnostic cartridge enclosure that must maintain hermetic sealing under pneumatic pressure testing.
-
Constraints: Biocompatibility requirements, optical clarity preservation, zero outgassing that could contaminate fluid channels.
-
Decision Points: Selecting high-intensity UV LED flood lamps versus focused spot-cure fiber optic delivery systems.
-
Failure Modes: Under-curing the adhesive at shadow zones where the opaque housing geometry blocks UV light penetration, leading to fluid leakage during diagnostic cycling.
-
Second-Order Effects: Redesigning the part geometry to incorporate energy-directing joint features ensures complete UV penetration, but requires expensive injection mold tooling modifications.
D : Architectural Structural Glazing
-
Context: Securing massive glass curtain wall panels to aluminum framing profiles using structural silicone sealants on high-rise skyscrapers.
-
Constraints: Wind load deflection, seismic drift tolerance, continuous solar ultraviolet radiation exposure.
-
Decision Points: Specifying two-part structural silicone with accelerated mixing versus moisture-cured single-component formulations requiring extended cure racks.
-
Failure Modes: Applying structural silicone onto aluminum frames with degraded or improperly applied organosilane primer, causing catastrophic panel detachment during high wind events.
-
Second-Order Effects: Mandating rigorous destructive peel testing on control coupons from every sealant batch guarantees boundary integrity, but introduces material waste and labor bottlenecks.
Planning, Cost, and Resource Dynamics
Preventing bond failures requires navigating direct expenditures, indirect operational costs, and hidden warranty liabilities. Many organizations falter because they evaluate adhesive bonding purely through the purchase price of the adhesive cartridge rather than total cost of ownership.
Direct costs include surface preparation chemicals, abrasive media, specialized priming equipment, and quality control testing labor. Indirect costs are more insidious: line stoppages caused by uncured adhesive batches, rework required to strip and re-bond defective assemblies, and warehouse climate control needed to maintain shelf-life stability for sensitive resins. Opportunity costs manifest when premature field failures damage brand reputation, resulting in expensive product recalls and lost contract bids.
| Cost Element | Reactive Approach (Fixing Failures) | Proactive Approach (Prevention) | Financial & Operational Impact |
| Surface Preparation | Minimal cleaning; relying on raw stock as-received | Automated plasma activation and precision solvent degreasing | Higher upfront capital; eliminates field failure warranty claims |
| Quality Control | Visual inspection of finished assemblies after cure | Destructive coupon testing and non-destructive optical gaging | Detects micro-defects early; prevents massive scrap lots |
| Material Handling | Ambient shop-floor storage with variable shelf life | Temperature-controlled cold storage and automated FIFO tracking | Reduces expired material waste and viscosity drift |
| Operator Training | Informal on-the-job shadowing and verbal instructions | Certified training programs on surface energy and mixing ratios | Lowers operator-induced mixing and application errors |
Managing variability remains a central challenge in adhesive planning. Ambient humidity, seasonal temperature shifts, and raw material batch variations from chemical suppliers can alter open times and cure kinetics. Robust planning frameworks incorporate dynamic operational buffers and strict environmental controls in bonding zones.
Tools, Strategies, and Support Systems
Deploying effective bonding processes requires a curated suite of technical tools and verification systems. Relying on visual inspection alone creates a dangerous illusion of quality.
-
Dynes Pens (Surface Energy Test Inks): Felt-tip applicators containing fluids of specific surface tensions used to quickly verify whether a substrate has achieved adequate surface energy (typically >38 dynes/cm) prior to bonding. Limits: Provides a semi-quantitative spot check rather than comprehensive surface mapping; can contaminate sensitive surfaces if misapplied.
-
Contact Angle Goniometers: Optical laboratory instruments that measure the droplet contact angle of liquids on a substrate to calculate exact surface free energy components. Limits: Destructive or off-line testing method unsuited for high-speed automated production lines.
-
Automated Meter-Mix-Dispense Systems: Closed-loop dispensing units equipped with dynamic or static mixers, real-time ratio monitoring, and automatic shutdown triggers if component ratios drift. Limits: Requires rigorous daily purging and regular maintenance seal replacements to prevent volumetric inaccuracies.
-
Non-Destructive Ultrasonic Testing: High-frequency sound wave analysis used to detect hidden voids, disbonds, or cohesive flaws within bonded lap joints without destroying the part. Limits: Operator-dependent interpretation; struggles with highly attenuating composite material matrices.
-
Environmental Chamber Testing: Accelerated weathering units that subject bonded test articles to extreme thermal shock, salt fog spray, and 100% relative humidity cycles. Limits: Accelerated tests model long-term aging but cannot perfectly replicate complex multi-factor real-world degradation.
-
Adhesive Primer Applicator Robots: Precision automated spray or wipe heads that deposit uniform, ultra-thin primer layers, eliminating human film-thickness variations. Limits: High capital investment and complex programming required for multi-axis component geometries.
Risk Landscape and Failure Modes
Every bonding intervention introduces technical vulnerability vectors. Understanding how adhesive systems fail prevents catastrophic structural incidents.
A primary risk is interfacial contamination drift. Over time, airborne silicones from lubricants, machining coolants, or release agents can settle on clean metal or plastic surfaces, forming an invisible monomolecular barrier that destroys wetting and causes instant adhesive delamination, even when standard cleaning protocols are ostensibly followed.
Another critical vulnerability is stoichiometric ratio error in multi-component adhesives. Epoxies and polyurethanes rely on precise chemical mixing ratios. If a dispensing machine drifts by even two percent, unreacted resin or hardener remains trapped in the matrix, drastically lowering glass transition temperatures and causing creep failure under sustained loads.
Compounding risks emerge when thermal management is ignored during exothermic cures. Fast-curing structural adhesives release significant heat; if applied in thick bead profiles without proper thermal dissipation, the exothermic spike can boil trapped moisture, create internal voids, and shatter the interfacial bond from within.
Governance, Maintenance, and Long-Term Adaptation
Achieving lasting operational stability depends on rigorous institutional governance. Without formal engineering controls, production lines frequently drift back to informal habits, improper surface preparation, and unmonitored shelf-life expiration.
Governance must begin with strict standard operating procedures embedded directly within shop-floor quality management systems. Maintenance of bonding infrastructure requires scheduled calibration cycles for dispensing meters, plasma generators, and cure ovens. Adjustment triggers should be clearly defined: if peel test coupon values drop below specified threshold limits for a single shift, the production line must automatically pause for root-cause analysis.
This cyclical feedback loop ensures that the operation adapts to seasonal humidity changes, new raw material batches, and equipment wear without compromising final joint integrity.
Measurement, Tracking, and Evaluation
You cannot manage what you do not measure, yet improper metrics can distort operational priorities. Evaluating adhesive integrity requires balancing leading and lagging indicators, as well as qualitative and quantitative signals.
-
Lagging Indicators: Field warranty claim rates for delamination, customer return percentages, and scrap rates identified during destructive post-cure testing. These metrics confirm past performance but offer no real-time protection.
-
Leading Indicators: Surface energy dynes test scores, component mix-ratio audit logs, ambient room humidity and temperature tracking, and open-time compliance metrics. These indicators catch process drift before parts leave the facility.
-
Qualitative Signals: Operator observations regarding adhesive viscosity changes, unusual odor shifts during mixing, or tactile changes in surface texture after cleaning wipes.
Documentation Examples
To maintain institutional clarity, manufacturing facilities should utilize standardized bonding documentation logs:
-
Surface Activation Log: Records surface energy dyne levels, plasma machine power settings, and solvent wipe lot numbers for every production lot.
-
Adhesive Batch Verification Sheet: Tracks resin and hardener expiration dates, lot numbers, storage temperatures, and meter-mix calibration test results.
-
Destructive Lap-Shear Coupon Report: Documents peak load failure values, failure mode classification (adhesive versus cohesive percentage), and environmental conditioning history for quality control test coupons.
Common Misconceptions and Oversimplifications
The technical discourse surrounding adhesive bonding and surface preparation contains persistent myths that undermine engineering reliability.
-
Myth: Wiping a surface with a solvent makes it chemically clean and ready for bonding.
-
Correction: Solvents often dissolve grease and smear it in a thin, invisible film across the surface rather than removing it entirely, unless a two-cloth wash-and-wipe technique with fresh solvent is rigorously enforced.
-
-
Myth: Higher clamp pressure always improves adhesive bond strength.
-
Correction: Excessive clamp pressure can squeeze out the adhesive entirely, starving the joint line and creating dry spots with zero structural contact.
-
-
Myth: All adhesives stick to all materials if given enough cure time.
-
Correction: Adhesives cannot form primary chemical bonds or mechanical interlocks with low-surface-energy polymers without prior corona, flame, or plasma surface activation.
-
-
Myth: Shelf-expired adhesives can still be used if they look and mix normally.
-
Correction: Expired resins and hardeners undergo molecular weight shifts and cross-linking degradation that compromise ultimate tensile strength and environmental durability, even if the liquid appears fluid.
-
-
Myth: Visual inspection is sufficient to confirm joint quality.
-
Correction: Interfacial contamination layers and microscopic boundary voids are completely invisible to the naked eye; non-destructive testing or destructive coupon sampling is mandatory for structural joints.
-
-
Myth: Curing at higher temperatures always accelerates bonding without negative side effects.
-
Correction: Rapid thermal curing can induce severe internal thermal stresses, cause boiling of volatile components, and distort thin-gauge substrates.
-
Ethical, Practical, and Contextual Considerations
Adhesive bonding and surface engineering do not operate in a vacuum; decisions regarding chemical selections and solvent cleaning carry profound environmental and occupational health dimensions.
The widespread use of volatile organic compound solvents for surface degreasing presents severe worker safety hazards and strict regulatory compliance challenges. Transitioning to aqueous cleaners or closed-loop plasma systems protects worker respiratory health and reduces hazardous air emissions. Furthermore, selecting structural adhesives that cannot be easily disassembled at end-of-life complicates circular economy mandates and recycling recovery pathways, requiring engineers to balance permanent bonding strength with future design-for-disassembly principles.
Practically, organizations must balance absolute cleanliness protocols with manufacturing velocity. Insist on over-engineered cleaning stations that slow down line speeds beyond economic viability, and the facility risks commercial failure; cut corners on surface preparation to boost throughput, and the risk of catastrophic field delamination multiplies exponentially. True engineering maturity lies in optimizing the boundary layer without sacrificing operational agility.
Conclusion
Mastering how to avoid poor adhesion problems demands a structural shift from empirical guesswork to rigorous surface physics and process governance. By examining historical precedents, applying robust mental frameworks, navigating material-specific trade-offs, and establishing closed-loop quality monitoring, operations teams can transform boundary bonding from a chronic point of failure into a reliable structural asset. True interfacial integrity is achieved not through brute-force adhesive selection, but through meticulous surface preparation, environmental control, and uncompromising process discipline.